End-to-end electronics design
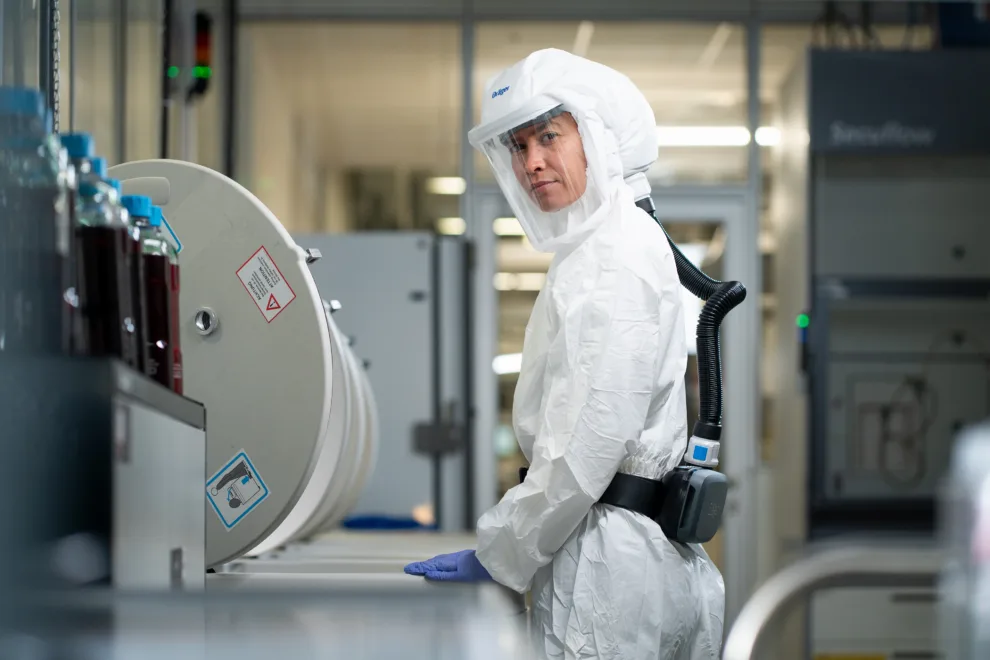
Whether supporting and augmenting your capabilities or taking the lead in working with manufacturers to bring the product to volume production, our in-house team of electronics engineers is capable of delivering the complete hardware design lifecycle. We can help you take products from initial ideas all the way to market, as we did, for example, with the Dräger X-plore 8300 pictured above.
Our design process has the rigour required for high-integrity designs, frequently in the medical sector, and the flexibility to allow faster and less formal development where appropriate.
We can undertake all the necessary development activities from initial requirements capture and architecture design through to pre-production prototypes and preparation for manufacturing handover, including schematic design, PCB layout, prototyping and testing in our electronics lab.

Architecture
Our approach is to establish the hardware architecture before starting the detailed design, avoiding locking in unnecessary cost and complexity.
The work required to define the right architecture may include power budget analysis; considering intrinsic safety; generating preliminary cost estimates; partitioning product functionality between mechanical, electronic and software sub-systems; early selection of major components; test planning or even performing practical feasibility studies and tests using development hardware rigs.
Architectural design was important in the early stages of the design of the Rolls Royce Future Systems Simulator, which had multiple complex systems working together. Initial consideration of how the system components would be distributed and the necessary communication links was vital to avoiding potential problems such as the risk of parasitic inductance and capacitance being introduced to high-speed signals over long cable runs.
Circuit design
This is where we finalise the selection of all the individual components for the electronic circuit design, populating the building blocks previously identified in the architectural design.
We use Altium tools for our electronic circuit design work and PCB layout activities. Following circuit design, we apply our ISO 9001 and ISO 13485 internal checking and review procedures to minimise the risk of circuit design iterations in later project stages, where changes are harder and more expensive to implement.
Selecting the most appropriate components from the outset can reduce bill of materials costs, which generates ongoing savings in volume production. We also review component availability as part of our circuit design release process, using our software tools to highlight any parts which are hard to obtain and should be reconsidered.

Analysis and simulation
If analysis and simulation tools are applied to the right elements of a circuit, they can save development time and accelerate the identification and avoidance of potential issues.
For one circuit requiring high precision control over a wide temperature range, we constructed such a simulation model based on a combination of circuit tolerance analysis and experimental data characterising the properties of an actuator. This allowed us to define the exact range of values over which the impedance of a bespoke metal element needed to be controlled, resulting in a solid calibration process and successful design testing.
Whether we are gauging anticipated battery life or fine-tuning the response of a filter, this theoretical modelling and simulation of circuit performance contributes to the early reduction of risk and a leaner development programme.
Reducing development risks and timescales
PCB layout
In-house PCB layout means that the engineer who designed the circuit can be intimately involved in seeing it through to realisation. Having the same engineers in charge of the circuit design and its realisation as a PCB assembly leads to better products as analogue signals are protected, signal integrity is managed on high-speed digital lines and potential EMC failures can be addressed at the source.
Our collection of component libraries and design rules based on IPC standards are periodically brought in line with up-to-date manufacturers’ capabilities. We have configured our Altium tools for automatic output and collation of standard manufacturing outputs, so we provide high quality manufacturing data packs suitable for prototype or volume manufacture.
We have rigorous procedures in place to give us a framework for the control of design data, maintaining consistency and quality across PCBA releases.

User interfaces
Selecting and implementing the right supporting hardware is a key part of achieving a good interaction experience for your user. Our electronics team works closely with our User Experience (UX) and software teams to design the user interface as a fully integrated whole.
When working on the TFT display for Linde we employed a low-cost hardware architecture to meet product cost targets, with clever use of a limited colour palette.
Even where the primary interface with a smart device is via an app, we have the expertise to maintain a high quality feel on the device itself. For the user interface on the Linn Selekt DSM product, we made early prototype PCBAs and rigs to evaluate how the LED indication lights and light guides would be implemented to give a uniform illumination intensity.
With our User Experience (UX) and software teams we can tailor the overall user interface system to deliver functionality, usability and desirability on the most cost effective and reliable hardware.

Motor drive and control
Our motor drive and control experience ranges from precision control of miniature motors at relatively low torque in medical devices, through to the higher torque requirements for industrial equipment such as the 3M and Dräger respiration systems, and even personal mobility systems.
Our experience is that the drivetrain must be designed as a full electromechanical system without division between the electrical motor and the mechanical components. An extra stage on the gearbox may take more space but will allow the motor to run at its most efficient speed, meaning it can be smaller, giving a more compact package overall.
Many of our motor drive solutions, like those listed above, are battery powered, requiring careful design to mitigate load transients on the battery and ensure performance is maintained across the whole battery charge cycle.

Product layout
It’s rare that a PCB can be designed with no consideration for the overall product layout.
Interactions with the casework, fixing methods and the positioning of electromechanical components, cables and interconnections all affect the electronic design, as illustrated in the X-plore 8300 shown here.
Our typical approach is to establish the approximate total board area required from the electronic architecture and work closely with the mechanical team using 3D CAD spatial models and physical block models to establish a rough layout. This highlights potential problems early on, such as a layout that requires long interconnection cables to allow the device to be assembled, which would then present a risk of EMC emissions problems. We exchange 3D data between electronic and mechanical CAD systems as the detailed design progresses to check for component clashes and can use Computational Fluid Dynamics to assess and address potential thermal issues. Continually reviewing the electro-mechanical interfaces is particularly important where the electronic systems are miniaturised for a small product size such as AllStar Connect.

Obsolescence management
All electronic systems use parts which will at some point become obsolete. This can cause a major problem, particularly where there has been a sizeable time and financial investment in certification.
One customer came to us with such a problem where the microcontroller in a safety-critical product was becoming obsolete with no drop-in replacement, but the embedded software had been through an extensive regulatory submission process. We found a solution that was implemented in the same physical space; some hardware functionality had to be moved external to the microcontroller but careful selection of the replacement meant this could be limited to simpler I/O with a contained and well-defined software change, which avoided the need for regulatory re-submission.
In other cases, manufacturers have come to us for a refresh of a product where many components are becoming old and expensive, or risking obsolescence. When Taylor Hobson approached us about a refresh of the Surtronic Duo, we were able to take a fresh look at the hardware architecture and design a new more economical and space efficient platform rather than replacing each component piecemeal.
Managing a substitution strategy to minimise the need for regulatory re-submission
Manufacturing transfer
We have worked with clients who have in-house manufacturing capability as well as with third-party manufacturing partners worldwide, and at varying scales of production volume.
Our typical approach when dealing with global manufacturers is to continue to take advantage of local prototyping channels for agile, small-scale builds while the design is evolving. A quick-turnaround prototype iteration of a design can be made in parallel with Design for Manufacture (DfM) refinement with the volume manufacturer, so the first volume prototype run is with a tested design.
We routinely get involved in defining and setting up manufacturing testing – in some cases producing some of the test equipment. Implementing embedded test software that runs on the PCBA and communicates with the manufacturing test set is commonly required, especially on smaller PCBAs where test points cannot be put on every net and traditional in-circuit test must be replaced with a functional test.